Overview
Combining Motherson’s KAVACH surface engineering with ceramic-bonded CBN substrates, MCB7005H (high-speed continuous finishing) and MCB7030H (heavy interrupted & impact turning) enable turning of hardened steels up to 65 HRC instead of cylindrical grinding.
Recommended Cutting Parameters (ISO H)
| Grade | ISO App. | Condition | Ap (mm) Ideal (Range) | Feed (mm/rev) Ideal | Vc (m/min) Min / Ideal / Max |
|---|---|---|---|---|---|
| MCB7005H | H05 | Continuous High-Speed | 0.12 (0.05–0.30) | 0.12 (0.05–0.50) | 130 / 170 / 250 |
| MCB7030H | H30 | Heavily Interrupted (Dry) | 0.20 (0.05–0.30) | 0.15 (0.05–0.50) | 50 / 120 / 180 |
Insert Range & Edge Preparations
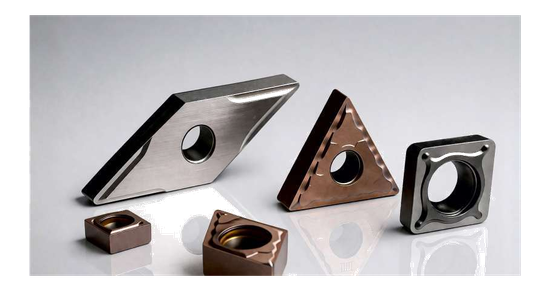
- Positive Inserts: CCGW, DCGW, TPGW, VBGW (STD, LS, WG, WH, HS edge preps)
- Negative Inserts: CNGA, DNGA, TNGA, VNGA, WNGA (2, 3, 4, and 6 CBN tips per insert)
Official Engineering Catalogues & Datasheets
Download both coated CBN grade brochures for continuous (H05) and interrupted (H30) cutting parameters and insert codes.